Blog
DOL Starters vs Star-Delta vs VFDs: The Complete Motor Control Selection Guide for UAE and Saudi Arabia

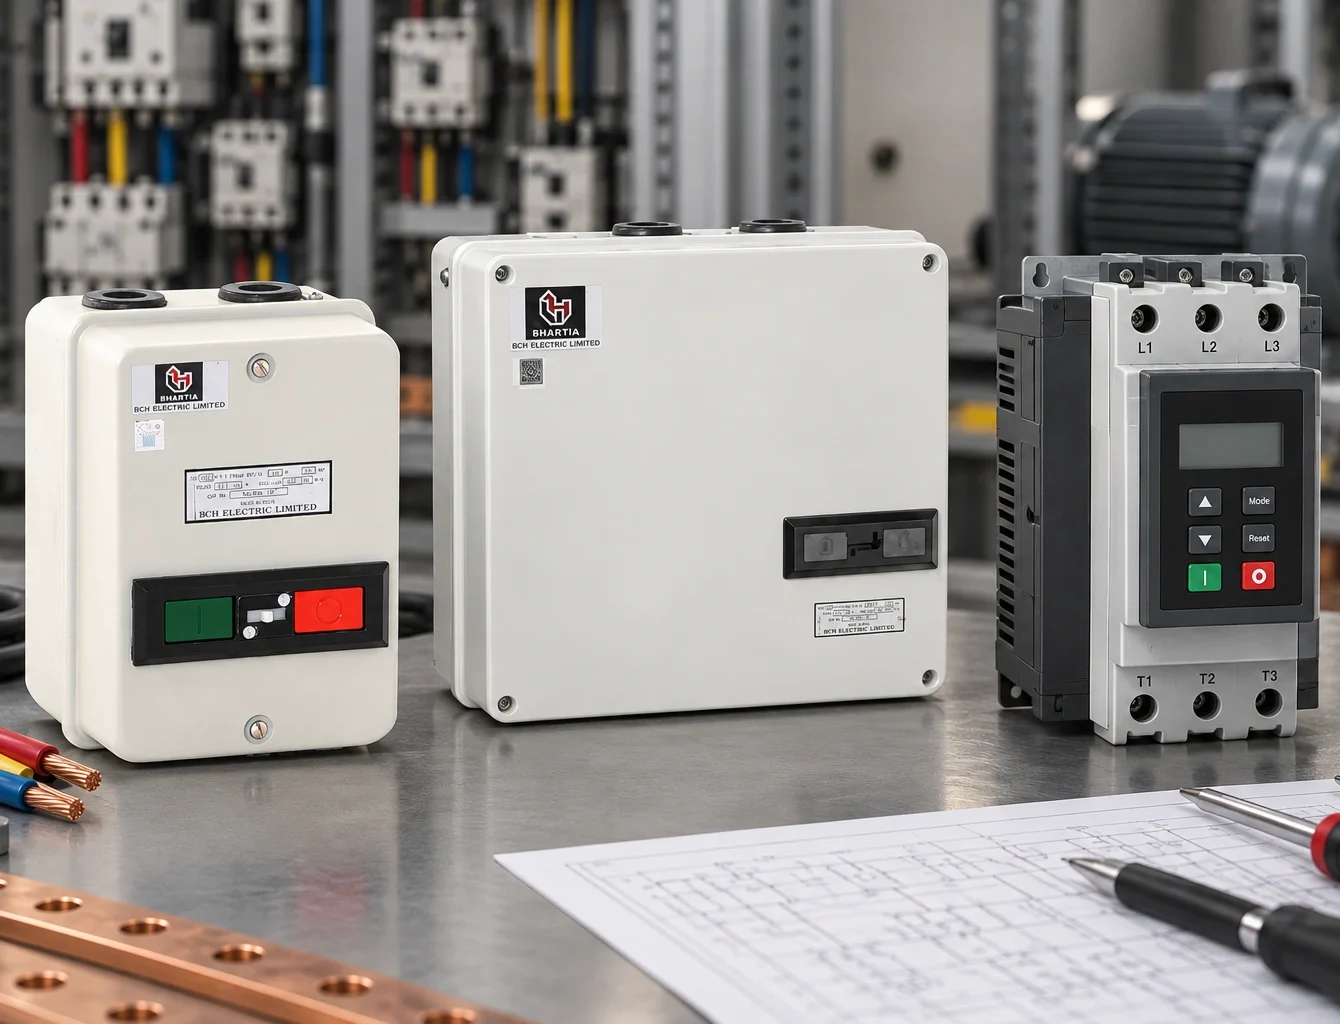
Every three-phase motor in a Gulf plant room, pump house or chiller yard runs behind one of three starting methods. Get the choice right and the motor runs for fifteen years on a maintenance schedule nobody thinks about. Get it wrong and you’re rewinding motors, replacing couplings, explaining kW-demand penalties to the finance team, or arguing with a utility inspector about why your 45 kW fire pump trips the incomer every Sunday morning. This guide walks through direct-on-line (DOL), star-delta and variable frequency drives (VFDs) as they actually behave in UAE and Saudi conditions — 50 Hz vs 60 Hz supply, 4550°C ambients, dust, and utility rules that don’t exist in the European textbooks most engineers learned from.
First, the regional context that changes the answer
Before comparing the three methods, four local realities need stating, because they shift the decision away from what a generic datasheet would suggest.
Frequency and voltage differ across the border. The UAE runs 50 Hz, typically 400 V for LV distribution. Saudi Arabia runs 60 Hz, with LV commonly at 380/400 V. This is not a footnote. A 4-pole motor turns roughly 1,450 rpm at 50 Hz and roughly 1,750 rpm at 60 Hz — about 20% faster. On a centrifugal pump or fan, affinity laws mean that same 20% speed increase pulls roughly 1.7 times the shaft power. Equipment specified for a Riyadh project and re-used in Dubai (or vice versa) without re-checking the duty point is one of the most common — and most expensive — regional mistakes. It also means a motor sized comfortably in one market can be badly overloaded in the other.
Ambient temperature eats your nameplate. Standard motor ratings assume 40°C ambient and 1,000 m altitude. A switchroom in Jubail or Al Ain in July does not resemble that. Above 40°C you derate: as a working rule, expect roughly 5% output loss at 45°C, around 10% at 50°C, and more beyond. VFDs derate harder than motors do, because the power electronics are the temperature-sensitive part — many drives lose 2–3% of continuous current rating per degree above their rated ambient, which is often 40°C or even 35°C for compact units. Panel ambient, not site ambient, is what matters, and a sealed IP55 panel in an unconditioned plant room can sit 15°C above the room.
Dust and humidity are design inputs, not weather. Fine desert dust is conductive when it picks up coastal humidity. It bridges contactor tips, blankets VFD heatsinks and clogs filter mats. Any comparison that ignores enclosure and cooling strategy is comparing brochures, not installations.
Efficiency compliance is enforced at customs. Saudi Arabia has mandated IE3 as the minimum efficiency class for in-scope single-speed three-phase cage induction motors, under SASO 2893, which is based on IEC 60034-30-1 and replaced the earlier SASO IEC 60034-30 standard. Motors need registration and a Certificate of Conformity to clear customs; motors fully integrated into a machine such as a pump or compressor are treated differently from stand-alone motors. In the UAE, motor efficiency and product conformity fall under MoIAT/ECAS requirements. Verify current scope and thresholds with SASO and MoIAT directly before you order — these lists get revised, and a non-compliant shipment sitting in Jeddah port is a schedule problem, not a paperwork problem.
Method 1: Direct-on-line (DOL)
The simplest possible arrangement — a contactor, an overload relay, a short-circuit protective device. Close the contactor, full voltage hits the motor terminals.
Starting current: roughly 6–8 times full-load current (FLC), for the whole acceleration period. Starting torque: 100% of design starting torque — typically 150–250% of full-load torque depending on the motor’s design class. Mechanical effect: the full torque impulse arrives instantly.
DOL is unbeatable on cost, panel footprint and reliability. There is almost nothing to fail. For small motors — exhaust fans, small transfer pumps, dampers, actuators, anything under roughly 5.5–7.5 kW — it is usually the correct answer and further sophistication is waste.
The problems begin as size grows. That 6–8× inrush causes a voltage dip across the supply impedance, which shows up as flickering lights, contactors dropping out elsewhere on the board, and VFDs or UPS units on the same bus registering undervoltage faults. On generator-backed supplies — extremely common on Gulf sites during commissioning, and standard on remote KSA installations — the dip is far worse because a genset’s source impedance is much higher than a transformer’s. A DOL start that’s invisible on utility power can stall a genset entirely.
Then there’s the mechanical side. Full torque applied instantly to a loaded belt drive shreds belts. On a long pipe run it produces water hammer, which cracks joints and destroys check valves. On a gearbox it takes a bite out of the fatigue life every single start.
Utilities in the region regulate this. DEWA, ADDC/AADC, SEWA, and the Saudi Electricity Company all impose limits on how large a motor may be started direct-on-line, and on permissible voltage dip at the point of common coupling. The thresholds vary by authority, by supply arrangement and by whether the connection is LV or HV, and they are revised periodically — check the current regulation for your specific authority and connection rather than relying on a number a colleague quoted from a project three years ago. Thepractical point stands regardless: above a certain size, DOL is not merely inadvisable, it’s not permitted.
Use DOL when: the motor is small, the load is low-inertia, starts are infrequent, and the supply is stiff.
Method 2: Star-delta (wye-delta)
Three contactors and a timer. Start with the windings in star, which puts roughly 58% of line voltage across each winding, then transition to delta for normal running.
Starting current: roughly one third of DOL — around 2–2.5× FLC. Starting torque: also roughly one third — and that is the entire problem. Requirement: the motor must be deltaconnected for its running voltage, with all six leads brought out to the terminal box. Not every motor is.
Star-delta earned its place because it solves the electrical problem cheaply. It reduces inrush by two thirds using components that cost a fraction of a drive and that any Gulf panel builder can source and repair in an afternoon.
But it does not solve the mechanical problem, and it introduces one of its own. Torque falls by the same factor as current, so the motor must be able to accelerate the load to near full speed on one third of its starting torque. On an unloaded centrifugal pump or a fan with closed dampers, fine. On a loaded conveyor, a screw compressor, a positive-displacement pump or anything with real breakaway torque, the motor stalls in star, sits there drawing heavy current, and cooks the windings or trips the overload.
The transition itself is the bigger risk. At changeover the motor briefly disconnects, and the residual voltage in the windings drifts out of phase with the supply. Reconnecting into delta at the wrong instant produces a current and torque transient that can exceed a plain DOL start — a violent jolt through the coupling and gearbox. This is why the open-transition star-delta starter, which is what most standard panels contain, is a mediocre soft-start. Closed-transition variants using a transition resistor bank suppress this, but they cost more and are rarer in regional standard panels than they should be.
Star-delta also has awkward interactions with modern efficiency requirements. IE3 and IE4 motors typically have higher inrush and lower rotor resistance than the older IE1/IE2 designs star-delta was tuned around, which can make the star-stage acceleration sluggish and the transition transient worse.
Star-delta remains the pragmatic middle for a specific band: medium motors, genuinely light or unloaded starts, cost-constrained projects, and situations where local maintenance capability is basic. Many Gulf clients still specify it by default for pumps in the 15–75 kW range. Often that default is defensible. Sometimes it’s just habit.
Use star-delta when: the motor is delta-capable, the load starts unloaded, inrush must come down, and budget or maintenance capability rules out a drive.
Method 3: Variable frequency drives (VFDs)
A VFD rectifies the incoming AC to DC and inverts it back to AC at a controlled voltage and frequency. It doesn’t just start the motor — it controls speed continuously.
Starting current: typically 100–150% of FLC. Often below full-load current. Starting torque: fully controllable, and available from zero speed. With vector control, you can hold 150% torque at standstill. Additional capability: continuous speed control, controlled deceleration, ramp profiles, soft stops, torque limiting, plus monitoring, energy metering and BMS communication.
The energy case is where VFDs justify themselves in this region, and the affinity laws do the arguing. For centrifugal loads — pumps, fans, chilled water systems, cooling towers, air handling units — flow varies with speed, but power varies with the cube of speed. Run at 80% speed and you use roughly half the power. Run at 50% and you use around an eighth.
Now consider what that means for Gulf HVAC. Chilled water and AHU systems dominate building electrical load here and spend most of their operating hours at part load — the peak-design condition of a July afternoon is a small fraction of annual hours. A throttling valve or damper that has been burning energy across a restriction all year is a straightforward retrofit candidate, and payback periods measured in months rather than years are realistic on large plant. This is exactly the logic behind efficiency programmes across the region, including Etihad ESCO’s retrofit work in Dubai and the Saudi Energy Efficiency Programme’s industrial motor initiatives.
There are real costs on the other side of the ledger. Harmonics. A standard 6-pulse VFD is a non-linear load that injects current harmonics — predominantly 5th and 7th — back into the supply. These heat transformers and neutrals, distort voltage for other equipment, and can cause nuisance tripping. Utilities here are increasingly explicit about it; DEWA and other regional authorities enforce harmonic limits at the point of common coupling, generally following IEEE 519 principles. Mitigation means line reactors or DC chokes for modest cases, passive or active harmonic filters for larger installations, or 12-/18-pulse and active front-end drives where distortion must be low. Budget for this at design stage. Discovering it during utility witness testing is expensive.
Motor stress. Fast-switching IGBTs produce steep voltage rise times. On long motor cables — and long runs are routine in Gulf plants where the switchroom sits far from the pump house — reflected wave phenomena can nearly double the voltage at the motor terminals,stressing winding insulation. Beyond roughly 50 m of cable, consider dV/dt filters or sine filters and specify inverter-duty motors with reinforced insulation. Separately, commonmode currents can discharge through the bearings and etch the raceways, a failure mode called electrical fluting. Shaft grounding rings or insulated non-drive-end bearings are the standard countermeasures, and they matter most on larger motors.
Heat and dust — the local killers. A VFD dissipates roughly 2–3% of its throughput as heat inside your panel. A 90 kW drive is a 2 kW heater. In a 45°C plant room that heat has to go somewhere, so panel cooling is not optional: forced ventilation with filters, panel air conditioners, or heat exchangers. Then the dust arrives. Clogged filter mats and dustblanketed heatsinks are the single most common cause of VFD failure in the Gulf, and they’re entirely preventable with a filter-replacement schedule. The failure is almost never the drive’s fault. It’s the maintenance regime’s.
Cooling degrades quietly. Blocked ventilation doesn’t announce itself. It raises internal temperature, which shortens DC bus capacitor life — capacitor life roughly halves for every 10°C rise — and the drive fails two years early for reasons nobody connects back to a €5 filter mat.
Use a VFD when: the load is variable, energy consumption is significant, process control benefits from speed variation, starting torque must be controlled precisely, or utility inrush limits leave no alternative.